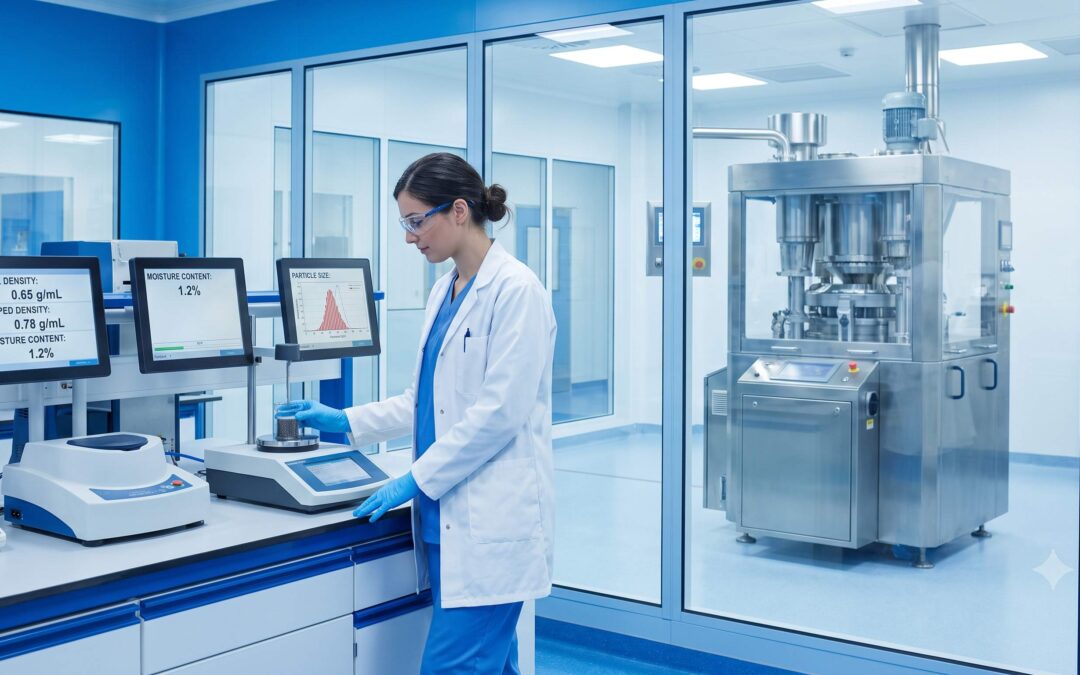
When a batch of pharmaceutical tablets fails in the compression room due to capping, lamination, or weight variation, the immediate reaction is often to adjust the machine settings or blame the rotary press.
However, experienced production and QA teams know that the root cause of these compression failures is rarely the press itself. Almost always, it lies upstream in granule density and consistency.
To achieve stable compression, predictable tablet hardness, and uniform weight, you must master the relationship between the physical properties of your granules before they ever reach the hopper.
🧪 1. Core Foundations: Bulk vs. Tapped Density
Granule packing behavior dictates downstream performance. Understanding these two values is critical for process control:
Bulk Density (Loose Density)
Measures the mass of the granules divided by their untapped volume (including the void spaces between particles). It represents how granules naturally pack under gravity as they fill the die.
Tapped Density (Packed Density)
Measured after mechanically tapping the granule bed until the volume becomes constant. It reflects the powder's ability to settle and pack under mechanical vibration or feeder force.
📊 2. Flowability Diagnostics: Carr’s Index & Hausner Ratio
By comparing loose bulk density and packed tapped density, you can calculate the flow and compressibility properties of your batch using two standard industry metrics:
Target: < 20% is preferred for good flow and stable compression. Values > 25% signal excess fines and irregular granule shapes, leading to poor flow and weight variation.
Target: < 1.25 is the gold standard for acceptable flow. A ratio > 1.25 indicates cohesive powder that will struggle to feed uniformly at high turret speeds.
⚡ When these values fluctuate during a run, your compression force will fluctuate rapidly, leading directly to weight and hardness variations.
⚙️ 3. Supporting Pillars: Moisture & Particle Size
Consistency goes beyond density. You must also maintain tight controls over:
Particle Size Distribution (PSD):
A delicate balance is required. Too many fines lead to air entrapment, capping, and lamination. Too many coarse particles result in poor packing and high weight variation. Standardizing your milling screen sizes is the key defensive step here.
Moisture Content (LOD):
Typically targeted within a 1.5% to 3.5% Loss on Drying (LOD) range. If granules are under-dried (high moisture), you will face sticking and picking on the punch faces. If over-dried (low moisture), the binder cannot form strong bonds, leading to weak, friable tablets.
📋 4. The GMP & Process Control Imperative
Global regulatory bodies (including WHO GMP, US FDA, EU GMP, and DGDA) emphasize that physical testing of granules—specifically bulk and tapped density—is a vital In-Process Control (IPC) and process validation step.
To safeguard your batches, build these preventive measures into your standard operating procedures:
- Control granulation endpoints and optimize wet-mixing times to prevent over-wetting.
- Standardize milling procedures (screen sizes and speeds) to control fines generation.
- Monitor drying endpoints closely to hit your exact formulation LOD target.
- Verify environmental humidity (keeping RH ≤ 50–60%) in manufacturing and compression suites to prevent moisture absorption or granule shrinkage.
- Run routine density trending to detect early-warning signs before they reach the tablet press.
The Key Takeaway
A stable, validated granulation process reduces downstream defects, protects your tablet tooling, and improves overall batch yields. Before you spend hours troubleshooting mechanical issues on your rotary press, look upstream to your granules.
Density is the ultimate predictor of tablet quality.